What Is the Difference Between 6010 and 6011 Welding Rods?
Both are cellulose-based, fast-freeze electrodes — but their flux composition and polarity options set them apart.
Both E6010 and E6011 are commonly used welding rods which are often confused for each other. Their difference lies in their last numerals, “0” and “1” which account for their different flux composition, slag type, and current type that can be used.
E6010 has a high cellulose sodium-type coating, whereas E6011 has a high cellulose potassium-type coating. Another major factor that separates their uses is that E6011 can run on both AC and DCEP models. Due to this, E6011 may have more uses in comparison to the other welding rods that run only on DCEP.
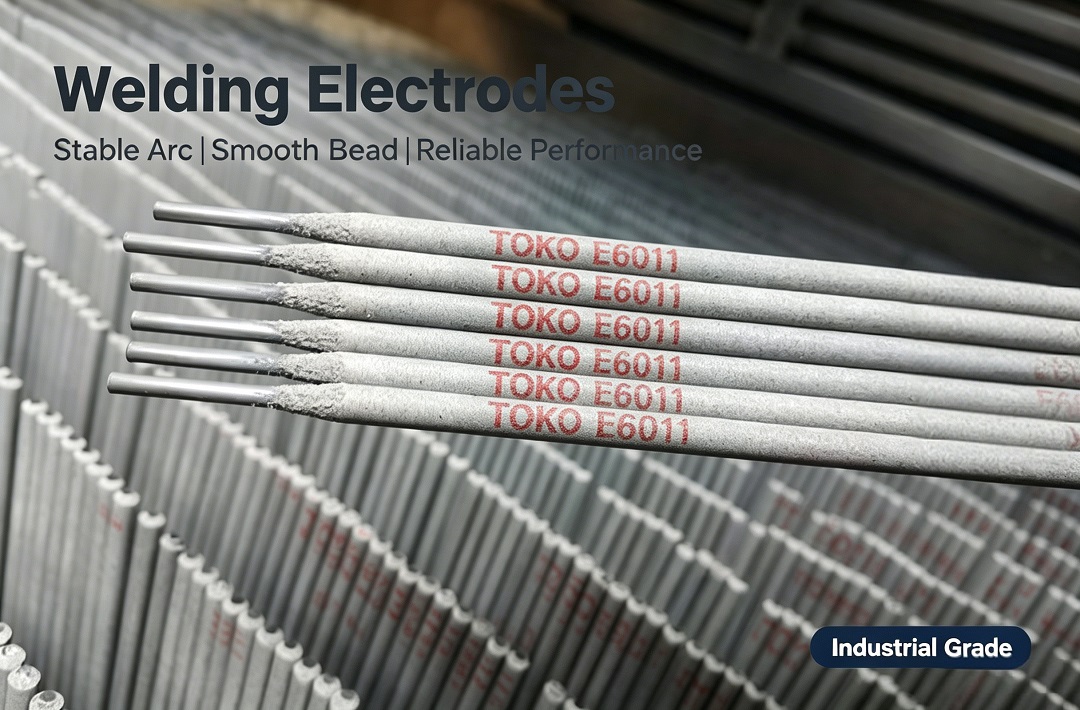
E6010 vs E6011 — Side by Side
| Property | TOKO E6010 | TOKO E6011 |
|---|---|---|
| Tensile Strength | 60,000 PSI | 60,000 PSI |
| Position | All positions | All positions |
| Polarity | DCEP | DCEP, DCEN, AC |
| Arc Characteristics | Violent, digging | Violent, digging |
| Flux Composition | Cellulose sodium (Fast Freeze) | Cellulose potassium (Fast Freeze) |
| Slag Type | Thin, flaky, does not peel | Thin, flaky, does not peel |
| Motion | Slight drag / Can whip (stitch) | Slight drag / Can whip (stitch) |
| Penetration | High | High (slightly deeper) |
⚡ Polarity Difference
Polarity results from an electrical circuit having either a negative or a positive pole.
E6010 electrodes are designed for DCEP (Direct Current Electrode Positive) only. On the other hand, E6011 can run on DCEP, DCEN, and AC sources. This makes E6011 a great "farm rod" for AC-only machines. Due to the flexibility of E6011, you can adjust and choose between polarities.
Even if you have a DC machine that can handle variable polarities, E6011 will not let you down in either circumstance.
🔽 Which Penetrates Better?
Unlike many other welding rods, both E6010 and E6011 have excellent penetration power. However, there is still a slight difference — E6011 has higher penetration and cleaning power in comparison to E6010.
You can assume the E6011 electrodes as a better version of the E6010 electrodes as it fulfills the need for all-purpose welding. Although E6011 is a better penetrator, the E6010 rod still has great penetration power and leaves just a little slag behind.
📍 All-Position Welding
Yes, both E6011 and E6010 can be run in flat, horizontal, vertical and overhead positions. The reason behind it is the fact that they do not produce a lot of slag, and they are fast-freeze rods.
As E6010 and E6011 are cellulosic electrodes, they're perfect for root passes, exclusively on DC+.
Both are very popular rods, mainly used where deep penetration is needed or in situations where you need to weld on contaminated surfaces like rust. Amongst professionals, E6010 is preferred for more critical projects like pipe welding, thanks to its better flux composition.
The information contained or otherwise referenced herein is presented only as "typical" without guarantee or warranty, and TOKO Corporation expressly disclaims any liability incurred from any reliance thereon. Typical data and test results for mechanical properties, deposit or electrode composition and other properties were obtained from a weld produced and tested according to prescribed standards, and should not be assumed to be the expected results in a particular application or weldment. Actual results will vary depending on many factors, including, but not limited to, weld procedure, plate chemistry and temperature, weldment design and fabrication methods. Users are cautioned to confirm by qualification testing, or other appropriate means, the suitability of any welding consumable and procedure before use in the intended application.