TOKO Tungsten Electrode — Precision TIG Welding
TOKO tungsten electrodes are manufactured from high-purity tungsten with carefully controlled oxide additions. They deliver stable arc characteristics, excellent ignition performance, and extended service life across a wide range of materials and welding positions.
Key Advantages
- High Melting Point (3422°C) — Withstands extreme heat without melting or degrading, ideal for high-current TIG welding.
- Excellent Electrical Conductivity — Ensures stable arc initiation and consistent weld quality with minimal arc wander.
- High Density & Low Vapor Pressure — Maintains a sharp tip for precise arc focus, producing clean, accurate welds.
- Durability & Longevity — Resists erosion and deformation, reducing electrode consumption and lowering welding costs.
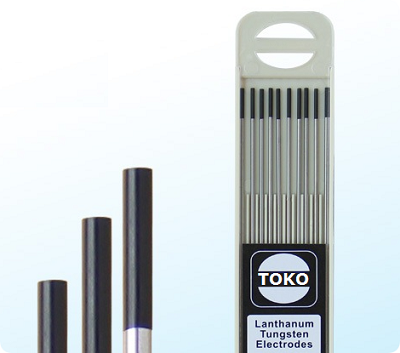
- Wide Range of Types & Sizes — Available in pure, thoriated, lanthanated, ceriated, and zirconiated variants; diameters from 1.0 mm to 6.0 mm.
Performance Benefits for TIG Welding
- Arc Stability: Smooth, focused arc even at low amperages — ideal for thin materials.
- Ignition Reliability: Easy, reliable arc starting with high-frequency or lift-arc systems.
- Tip Life: Superior resistance to spitting and balling, reducing regrinding frequency.
- Versatility: Compatible with AC, DCEN, and DCEP polarities across a wide current range.
- Weld Quality: Produces contamination-free welds with excellent penetration control.
Tungsten Electrode Types — Choose by Application
Each type is identified by a distinctive end color for easy recognition.
Pure Tungsten (WP)
Color: Green
Excellent for AC welding of aluminum and magnesium. Good arc stability with low current.
Thoriated 2% (WT20)
Color: Red
Best for DC welding of carbon steel, stainless, and nickel alloys. Excellent ignition and long life.
Lanthanated 1.5% (WL15)
Color: Gold
Versatile for AC/DC, low current. Excellent arc stability, low erosion, no radioactive hazard.
Lanthanated 2% (WL20)
Color: Blue
Superior arc stability, high current capacity. Ideal for both AC and DC welding of all materials.
Ceriated 2% (WC20)
Color: Orange
Excellent low-current performance, good arc starting. Suitable for DC and AC welding of thin sections.
Zirconiated (WZ8)
Color: White
Optimized for AC welding of aluminum and magnesium. Resists contamination and maintains balled tip.
Primary Applications
TOKO tungsten electrodes are trusted across demanding industries worldwide.
Heavy Fabrication
Shipbuilding, pressure vessels, structural steel — high-current DC welding with thoriated or lanthanated types.
Aerospace & Defense
Precision welding of titanium, Inconel, and superalloys. Lanthanated and ceriated electrodes ensure zero contamination.
Automotive
Exhaust systems, chassis components, aluminum panels — AC welding with pure or zirconiated electrodes.
Energy & Power
Boilers, heat exchangers, turbine components — high-reliability welds with thoriated or lanthanated electrodes.
Additional Applications
- Pipe and tube welding (stainless, carbon, alloy)
- Aluminum and magnesium fabrication
- Maintenance and repair welding
- Orbital tube welding systems
- Research and development laboratories
- Art and architectural metalwork

Technical Specifications
Chemical Composition (Typical)
| Element / Oxide | Pure (WP) | Thoriated (WT20) | Lanthanated (WL20) | Ceriated (WC20) |
|---|---|---|---|---|
| Tungsten (W) % | ≥99.95 | 97.80 | 97.80 | 97.80 |
| ThO₂ % | — | 1.8 – 2.2 | — | — |
| La₂O₃ % | — | — | 1.8 – 2.2 | — |
| CeO₂ % | — | — | — | 1.8 – 2.2 |
| Impurities % | ≤0.05 | ≤0.05 | ≤0.05 | ≤0.05 |
Physical Properties
| Property | Value |
|---|---|
| Melting Point | 3422°C (6192°F) |
| Density | 19.3 g/cm³ |
| Electrical Conductivity | ~18% IACS |
| Thermal Conductivity | 174 W/(m·K) |
| Vapor Pressure @ 3000°C | ~10⁻⁴ Pa |
Available Diameters & Lengths
| Diameter (mm) | Diameter (inch) | Standard Length (mm) |
|---|---|---|
| 1.0 | 0.040" | 150 / 175 |
| 1.6 | 1/16" | 150 / 175 |
| 2.0 | 5/64" | 150 / 175 |
| 2.4 | 3/32" | 150 / 175 |
| 3.2 | 1/8" | 150 / 175 |
| 4.0 | 5/32" | 150 / 175 |
| 4.8 | 3/16" | 150 / 175 |
| 6.0 | 1/4" | 150 / 175 |
Recommended Current Ranges (DCEN, Argon Shield)
| Diameter (mm) | Current Range (A) | Typical Application |
|---|---|---|
| 1.0 | 30 – 60 | Thin sheet, precision work |
| 1.6 | 60 – 120 | General purpose, light fabrication |
| 2.4 | 120 – 200 | Medium thickness, structural |
| 3.2 | 200 – 300 | Heavy plate, high deposition |
| 4.0 | 280 – 400 | Heavy fabrication, thick sections |
For AC welding of aluminum, reduce current by 20–30% and use pure, zirconiated, or lanthanated types.
Certifications & Technical Docs
Download material certificates, SDS, and TIG welding procedure guidelines for TOKO tungsten electrodes.
All certifications comply with AWS A5.12 / ASME SFA-5.12 and ISO 6848.