TOKO AWS A5.1 E6013 Rutile Welding Electrode
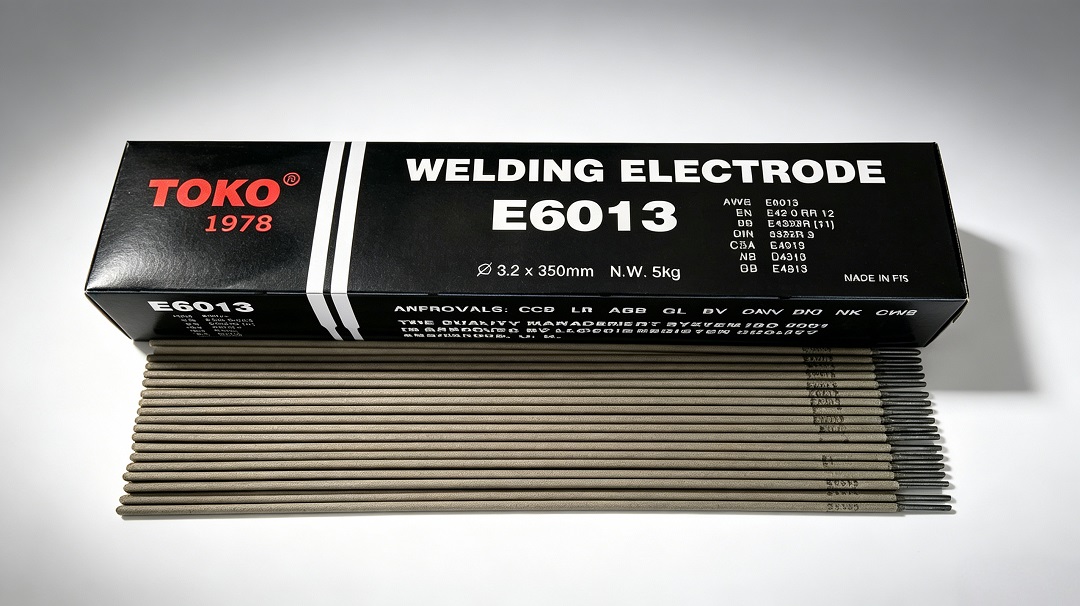
Rutile-coated electrode designed for single- and multi-pass welding of mild and low-carbon steels. Combines smooth arc characteristics, easy slag removal, and excellent bead appearance for general fabrication and repair.
Key Advantages
- AWS A5.1 / SFA-5.1 compliant — full traceability and certified mechanicals.
- Rutile-based coating — provides smooth arc, easy restrike, and low spatter.
- All-position capability — flat, horizontal, vertical-up, and overhead.
- Forgiving on surface conditions — works well on rusty, painted, or slightly dirty steel.
- Excellent bead appearance — produces fine ripple and smooth finish.
- Available diameters: 2.5mm (3/32"), 3.2mm (1/8"), 4.0mm (5/32"), 5.0mm (3/16").
Performance Benefits for General Fabrication
- Arc Stability: Smooth, stable arc with minimal spatter on AC or DC.
- Slag Removal: Self-detaching slag, reducing cleanup time.
- Weld Appearance: Fine, uniform ripples with minimal undercut.
- Easy Operation: Excellent for out-of-position welding, even for beginners.
- Versatility: Ideal for sheet metal to medium plate, single or multi-pass.
Primary Industrial Applications
Trusted in workshops, construction sites, and repair shops worldwide.
General Fabrication
Light structural steel, frames, brackets, and supports — quick and clean.
Automotive & Sheet Metal
Body panels, exhaust systems, and thin-gauge repairs with minimal burn-through.
Maintenance & Repair
Farm equipment, machinery, and field repairs — forgiving on dirty surfaces.
Light Construction
Handrails, gates, fencing, and ornamental iron work.
Additional Applications
- Pipe welding (non-critical)
- Furniture manufacturing
- DIY projects and hobby welding
- Shipbuilding interior fittings
- Storage tank fabrication
Technical Specifications
Chemical Composition (Typical, Weld Metal)
| Element | Value (%) |
|---|---|
| Carbon (C) | 0.06 – 0.12 |
| Manganese (Mn) | 0.40 – 0.70 |
| Silicon (Si) | 0.15 – 0.35 |
| Phosphorus (P) | ≤ 0.025 |
| Sulfur (S) | ≤ 0.020 |
Mechanical Properties (As-Welded)
| Property | Value |
|---|---|
| Tensile Strength (MPa) | 440 – 540 |
| Yield Strength (MPa) | ≥ 350 |
| Elongation (%) | ≥ 20 |
| Charpy V-notch @ 0°C (J) | ≥ 27 (typical 40-60) |
Welding Parameters (AC/DC+)
| Diameter (mm) | Current (A) | Voltage (V) |
|---|---|---|
| 2.5 | 60 – 100 | 21 – 23 |
| 3.2 | 90 – 140 | 22 – 25 |
| 4.0 | 130 – 180 | 24 – 27 |
| 5.0 | 170 – 240 | 25 – 29 |
AC or DC+ suitable; DC+ gives slightly smoother arc.
Storage & Re-drying
| Condition | Requirement |
|---|---|
| Unopened packaging | Store in dry place (<60% RH) |
| Opened electrodes | Use within 8 hours or store at 80-120°C |
| Re-drying (if damp) | 250-300°C for 1 hour |
Certifications & Technical Docs
Download batch-specific material certificates, SDS, and welding procedure guidelines.
All certifications are third-party verified and comply with AWS A5.1 / ASME SFA-5.1.